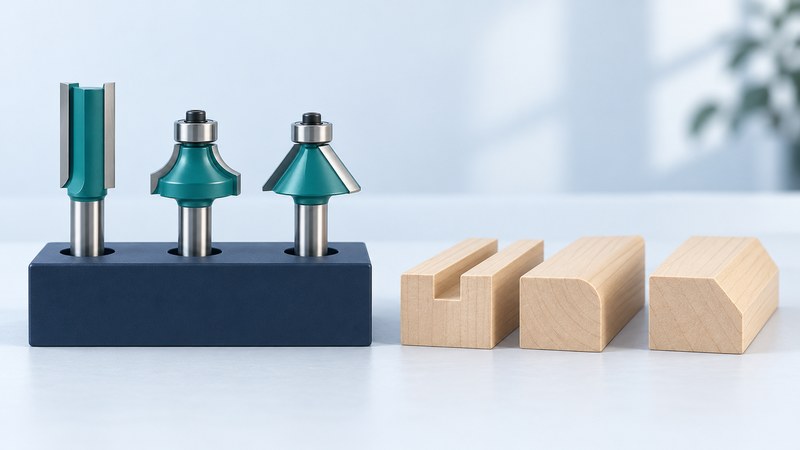
Choose the finished shape before the set
Draw the edge or joint you want and identify its dimensions. A small collection selected for actual projects is easier to understand than a large assortment of unfamiliar cutters. Freud’s routing-tool categories distinguish straight, trimming, edge-forming and joinery applications; the exact bit specification still determines its permitted use.
| Intended result | Family to investigate | Detail to verify |
|---|---|---|
| Straight groove or recess | Straight or suitable spiral bit | Cutting diameter, depth and whether plunging is permitted. |
| Trim to an edge or template | Flush-trim or pattern bit | Bearing location, template thickness and cutting length. |
| Soften or bevel an edge | Roundover or chamfer bit | Radius or angle and the remaining supported edge. |
| Form a mating joint | Matched joinery cutters | Stock thickness range, setup sequence and table requirement. |
Measure the actual stock. Material sold with a nominal thickness may not match the dimension a joint needs. For rail-and-stile work, treat the matched cutters, stock thickness and setup instructions as one system. A visually similar profile from another bit may not make the mating joint.
Match shank, collet and cutting envelope
The shank is the smooth portion held by the collet. Use the exact shank size and an approved collet or reducer for the router. A 1/4-inch shank is 6.35 mm, so it is not interchangeable with a 6 mm shank. Check cutting diameter, cutting length and clearance through the base or table insert separately.
Freud’s safe-working instructions (PDF) require compatible clamping dimensions, the minimum clamping length and observance of marked speed limits. Keep clamping surfaces clean and use the specified tightening method. Never extend a bit by gripping only a small part of its shank; follow the bit and router instructions for insertion and bottom clearance.
Check for chipped carbide, cracks, bent shanks or a damaged bearing before mounting. Remove questionable tooling from service. Use the maker’s approved replacement bearing and fasteners; a bearing change can alter both guidance and the cut. Disconnect the power supply before inspecting or changing the setup.
Find the operating limits for this combination
A maximum RPM is a ceiling, not a recommended setting for every cut. Identify the bit’s permitted speed range, the router’s settings and any table-only restriction. Respect the lowest applicable maximum among the equipment and accessories, while remaining within all specified operating ranges. If there is no compatible range, change the combination.
Do not infer safety from a phrase such as “anti-kickback” or from a cutter’s coating. Guidance, work support, depth and feed still matter. Large profiles and joinery cutters can require a table or other specified fixture; a bit that fits the collet may still be unsuitable for handheld operation.
Write down the bit part number and its instructions before discarding the packaging. This makes the operating limits recoverable months later, when a loose cutter in a drawer no longer has an obvious identity.
Use a test piece that represents the real cut
- Choose scrap matching the actual material and thickness. Mark the reference face, intended profile and waste area.
- Plan guidance with the router base, fence, bearing or template as appropriate. Secure the work and confirm the cutter can start clear of it.
- Set a permitted speed and a conservative pass sequence from the equipment instructions. Use eye and hearing protection and the required dust controls.
- Make the test cut, switch off and wait for the cutter to stop before inspecting. Check dimensions and fit with the mating piece.
- Disconnect power before adjustment. Retest after changing height, guidance or pass depth, then preserve the successful sample.
CCOHS router guidance recommends matching scrap for setting depth and passes, securing the stock and retaining control until the motor stops. Feed against cutter rotation as directed for the specific operation. Handheld and table arrangements move different parts of the system; use the router-table guide for table setup.
Diagnose a poor cut before changing the speed
A burnt surface can reflect several problems: dull or dirty cutting edges, excessive rubbing, feed or an unsuitable setting. Tear-out may involve grain direction, unsupported fibers or too much material removal. Stop and inspect rather than assuming one speed change fixes every defect.
Keep a sample labeled with bit identity, stock thickness, reference face and relevant settings. Clean and store bits according to their manufacturer, with cutting edges protected from collision. Professional sharpening or replacement is appropriate when damage or wear prevents a reliable cut; do not reshape carbide or alter the shank to make an incompatible bit fit.
Choose your next guide
- Router Tables — Plan work support, guarding and a controlled routing setup.
- Wood Rasps — Explore hand shaping for curves, edges and fitted parts.
- Cordless Rotary Tools — Match small rotary accessories to the task and speed range.
Browse woodworking and shaping or explore all 47 tool guides.