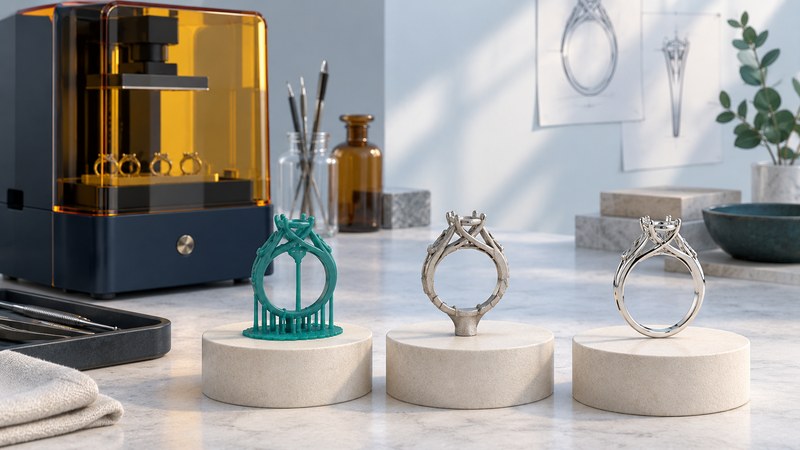
Choose a jewelry 3D-printing process by the cast and finished features it can reliably deliver. A sharp-looking pattern is an intermediate result. Give the printer supplier and foundry the same representative design, final requirements and trial record so they can trace defects through the complete route.
Choose a trial that represents the jewelry
Select features that drive acceptance: stone seats, prongs, filigree, engraving, ring dimensions and surfaces that must polish cleanly. Identify accessible inspection locations and distinguish dimensional requirements from visual references. Include a difficult representative feature alongside an easier control.
Ask for the proposed process and material by exact name. A wax pattern and a wax-filled photopolymer pattern have different processing instructions. Printer layer height describes one aspect of a build; assess the actual feature in its intended orientation and after supports are removed.
Arrange supports and casting sprues with the appropriate specialists. Printing supports hold the part during manufacture; casting sprues provide the route used during casting. Their locations and removal stages serve different purposes and can affect different surfaces.
Use the material's complete processing route
Formlabs' Castable Wax instructions illustrate why material identity matters: that named resin requires washing and drying but does not require post-curing. The same instructions warn that post-curing can affect dimensions. Other casting resins have their own requirements. Obtain the current route for the selected material, printer and investment.
Record the build, cleaning, drying, support-removal and any required cure steps. Keep patterns identified through shared trays and outsourced casting. Agree with the foundry on the investment, alloy, flask configuration and burnout documentation before printing the trial.
The manufacturer's jewelry casting guide ties burnout to investment, flask and pattern conditions. Use current applicable supplier instructions and the foundry's qualified process. Furnace, ventilation, molten-metal and chemical operations belong to trained personnel using the actual equipment procedures and safety information.
Inspect at three stages
On a narrow screen, scroll the table horizontally. Keyboard users can focus it and use the arrow keys.
| Stage | Inspect | Question answered |
|---|---|---|
| Prepared pattern | Dimensions, support scars, missing features and surface residue | What entered the foundry? |
| As-cast part | Same accessible features, fill and surface condition | What changed during casting and initial cleanup? |
| Finished piece | Final dimensions, seats, edges and appearance | What can be accepted for the intended jewelry? |
Use a consistent measurement method, datum and part condition at each stage. Photograph defects before finishing removes evidence. Where porosity or internal integrity matters, agree on the inspection method with the foundry rather than relying on an exterior photograph.
Fictional feature: a width measures 2.10 mm on the prepared pattern, 2.04 mm as cast and 2.00 mm after finishing. The observed changes are −0.06 mm during the casting stage and −0.04 mm during finishing, totaling −0.10 mm.
That sequence directs the investigation to two stages. It does not establish a universal shrinkage allowance: repeat representative geometries and orientations before changing the design scale.
Compare accepted results and the work needed
For each candidate route, report accepted pieces, rejected features, repair work and finishing time. Separate build failures from casting and finishing losses. A rapid print that creates difficult polishing work may change the overall production decision.
When a defect appears, retain the accepted control and alter one planned factor. Recheck the features that previously passed. Record the final qualified route with supplier document revisions and the reason to revisit it after a material or equipment change.
For general planning, see rapid prototyping. Use the SLA post-curing guide where the selected material calls for that step; the exact casting-material instructions determine its place in this route.
Use the working record
Download the editable jewelry pattern trial. Save a copy, complete the actual requirements and evidence fields, and review open issues with the responsible owner. The plain-text record includes instructions, units where needed, the fictional example, and source references.